Showing posts with label Card Clothing. Show all posts

Metallic wire specifications – Card Clothing

The specifications for metallic card clothing suitable for medium staple 26 to 30 mm and less than 5% trash

clip_image001

Where, Fibre Length Micronaire Bale trash

A - Below 26mm. Above 4 Above 5%

B - 26 to 30mm. 3. 7 to 4 Below 5%

C - Above 30mm. Below 3. 7 Below 4%

D- Bleached Cotton and Waste Cotton.

E - Svnthetic Fibres. (38 to 60mm. & upto 2 denier)

Read more...

Objects and methods of grinding in Carding Machine.

It includes the following topics

1. Object of grinding.

2. Metallic wire grinding procedure.

3. Grinding Roller

Object of grinding:

As a card operates, the action of fibres and dirt with it, gradually wear the points of wire causing them to become poor  cleaning point. The purpose of card grinding is to maintain the card clothing in a sharp condition.

Metallic wire grinding procedure

Cleaning the card:

Remove the lap and strip the cylinder & doffer

Run the card until all the flats are stripped out

Remove the flat strips

Remove all the trash from under the card for they may cause a fire.

preparing for grinding:

Take off the main belt and guide.

Remove the doffer driving belt and dis engage the doffer driving gear.

Remove the flat driving belt. Br Remove the belt from cylinder to lickerin. -   Disengage the calender roller drive,

Remove the doffer comb bands. - Replace the main belt and guide to drive the cylinder back wards (in opposite direction) most motors are fitted with reversing starters and the change of direction can usually be obtained by means of special key.

Connect the cylinder and doffer pulleys with an open belt.

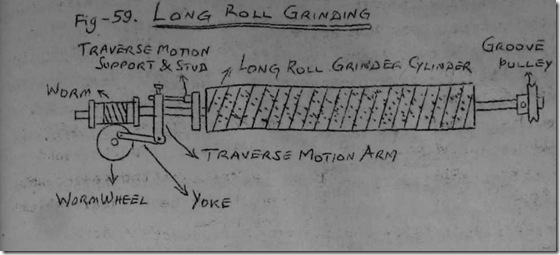
put the grinding roll in the cylinder stand with the driving pulley on the opposite side from the main driving belt.

Put on the grinding band to drive the grinding roll, so that they turn in the same direction as the cylinder. This causes the surface of the emery covered roll to run against the back of the card wire.

In the case of fast grinding, the driving connection is given as shown in the figure, assuming the cylinder speed of 170 rpm then,

Grinding Roll speed = 170 x (18/4) =755
Doffer speed =170 x (18/12) =255 RPM

In the case of slow grinding the following driving connection is given as shown in the fig.

Assuming 170 RPM as the speed of the loose pulley on the cylinder shaft, then Doffer =(170 x(16/95) x (5/100) x (40/216) =13. 2 RPM

clip_image042

Cylinder =13. 2 x (2 / 18) =8. 8 RPM

Grinding roller =170 x (16/9. 5)x (9. 5/4) =680 RPM

Start the card -The card is now so arranged that the cylinder,

doffer and grinding roller are the only parts moving.

Brush out the cylinder very care fully by holding the brush firmly and press it into the wire of the moving cylinder.

Stop the card and lift & correct any bent or jammed wire with special hook.

Before grinding, the setting should be noted so that an indication of amount of wire height removed by grinding can be obtained, when these settings are re-checked after grinding,

DURING GRINDING

Start the card running, listening for contacts. If either grinding roll touches it will cause a brushing sound.

Set the grinding roll down gradually until slightly brushing -action is heard.

The adjusting of the grinding roll during grinding against the cylinder is usually a matter of judgement.

Spark should not exceed 50 mm on cylinder and 30 mm on doffer.

Set the grind stone about 0. 15 mm clear off the surface of the wire at each end of traverse.

After 6-8 min, stop the grinding and the sharpness of wire points should be examined through micros cope. The presence of serrations on the wire and majority of points showing clear grinding, striations with a fine burr at the leading edge can be taken as an indication that the grinding has been done well.

Worn out grinding stone & deep meshing of grinding stone on wire would break or damage the wire and may lead to hooked or bent wire points.

The grinding stone used in grinding a card is aluminium oxide vitrified bond 46/L 7v or WA 80 /PE 31. It is a emery having a granular formation.

Starting up after grinding:

Remove the grinding band and Roller Remove the belt from cylinder to doffer Engage all the card drive connection as usual Reset all the settings Put on the main belt and bring the normal direction to cylinder after grinding. Turn the card parts by hand and listen for any contacts of surfaces. tart the card care fully and listen for contacts

Put the lap and reengage the side shaft gear

Start the calender roll when the web is in good shape.

Discard the first few yards of sliver on account of dirt and light weight.

img31

Grinding Frequency;

Generally, grinding of cylinder and doffer should be carried out once in 6 month or after taking 40000 kg production and card should be reclothed once in 3 to 4 year or after 1. 5 lakhs kg production in one card.

Generally frequency of grinding depends upon the rate of production, quality of material, type of wire points and level of neps in the cad web.

Read more...

Card clothing-Flexible and Metallic clothing and their specifications and their merits and demerits

Study of card clothing may be broadly classified into the
following heads:

1. Comparison between flexible and metallic wire clothing.

2. Metallic wire specifications

3. Metallic wire clothing procedure.

comparison between flexible and Metallic wire clothing

Limitations of conventional revolving flat card clothed flexible wires are

The conventional carding efficiency is very, much effected due to frequent stoppages for stripping and grinding. Further, the regularity of the sliver is much affected after every stripping.

Condition of the wire point increases the waste% and neps formation.

Foundation of the flexible wire clothing is not regid and fails to bare the stress and strain caused by high speed, so cannot be run at high speed.

So, In semi high production card, the efficiency of the card is improved by replacement of flexible wire with rigid wire clothing known as metallic wire clothing.

Metallic wire clothing on cylinder and doffer gives the following advantages over the flexible fillets :

1. Reduction in stripping cycles-once in 2 or 3 days

2. No frequent grinding-only light grinding at an interval of 6 months on 3 shift basis.

3. The above two advantages go in favour of more production &

regularity of sliver is improved & labour work is reduced.

4, NO neps formation due to better wire condition,

5, Saving of good fibres.

Lesser variation in card sliver owing to reduced stripping cycles.

Card can run at high speed owing to rigid foundation of wires.

Economic in long run.

some of the demerits of metallic clothing are:

less fibre holding power

It shows slightly higher fibre damage.

High fly generation.

Requires higher power consumption.

Greater care in maintenance and attention owing closer gauging and setting.

It is difficult to replace the damaged wire portion only. (Damaged portion only can be replaced in flexible fillet clothing).

Metallic wire clothing procedure.

How is a card clothed with metallic wires How the ordinary Flat card is prepared before covering with metallic wires.

Following procedure is adopted before the Metallic wire clothing

Check the level of the frame and alignment of cyliner and doffer. Dynamically balance the lickerin, cylinder and doffer.

Metallic clothing demands closer setting than flexible clothing. So, accurate mountaining is essential for successful mountaing.

The cylinder surface is ground before mounting the metallic wire to get even surface.

Ensure that there is a gap of 1" between bare cylinder and doffer

Metallic wire has less than half the height of flexible card clothing. Therfore when a conventional card of lesser diameter cylinder is converted for metallic clothing, the diameter of cylinder and doffer have to be built up, by mounting a base wire of about 4.5 mm in height an 1.5 mm in width. So, the procedure for clothing old lesser diameter cylinder differs slightly from new larger diameter cylinder.

In the case of cards having lesser diameter of cylinder, the following procedure is adopted.

clip_image0202

Fig A: Grooving of cylinder to fix L wire on both the edge of cylinder & doffer.

Pig B: Cut the groove with care and fix L wire to the exact dimension,

Fig C: Grooving of L wire to fix the bead wire.

Fig D: Mounting of base wire across the width by using wire mounting equipment is ground.

Base wire is ground by using traverse grinder with grindstone -Wa 36/46 J.V.L.P or A 46/L7v Fig E: mounting of bead wire into the groove already cut on the L-wire.

Fig F Mounting of Metallic wire across the width by using
wire mounting equipment.

L wire is fixed to maintain the position of base wire and bead wire is mounted to maintain the position of metallic wire at the edge of cylinder and doffer and prevent the coming out of wire from the edge of cylinder and doffer.

In the case of card having larger diameter of cylinder. The following procedure is adopted:

clip_image2004

Fig G: Grooving of cylinder to fix z wire on both the edge I Fig h: Mounting of z wire

Fig I: Mounting of metallic wire across the width by using wire mounting equipment.

z wire is used on larger diameter cylinder where no base wire is needed.

Metallic wire mounting procedure:

Make a saw cut in the bead or z wire. Bend the metallic wire and insert into the saw cut made in the bead or Z wire. Hammer round the bent portion to form a fine'U' .

With the wire thus attached, bring the pressure arm to the extreme right hand edge.

Place the supply spool of new metallic wire in its creel and thread the wire through tension plate, forming Roller & pressure Roller to the mounting apparatus as shown in Fig.

clip_image0402

When commencing to wind, the first few Revolutions should be I wound slowly by hand.

The speed may then be increased upto 16 R.P.M. continue to wind on to the cylinder until the wire nearer the left hand edge, at last solder the wire to ensure the sound joint on each side of cylinder or doffer. After clothing:

Any grease or waxy substances from the wire surface should be removed by washing the wire with petrol or carbon tetra chloride.

The wire Should now be ground for 20 min then burnished for 10 min atlast again ground for 10 min for square off and clean up the point to give a clean carding point under the microscope.

Read more...